
ID SOLUTECH / CNC MACHINING
PRODUCT BRIEF · CNC 19
중공 플랜지 샤프트
Hollow flanged shafts
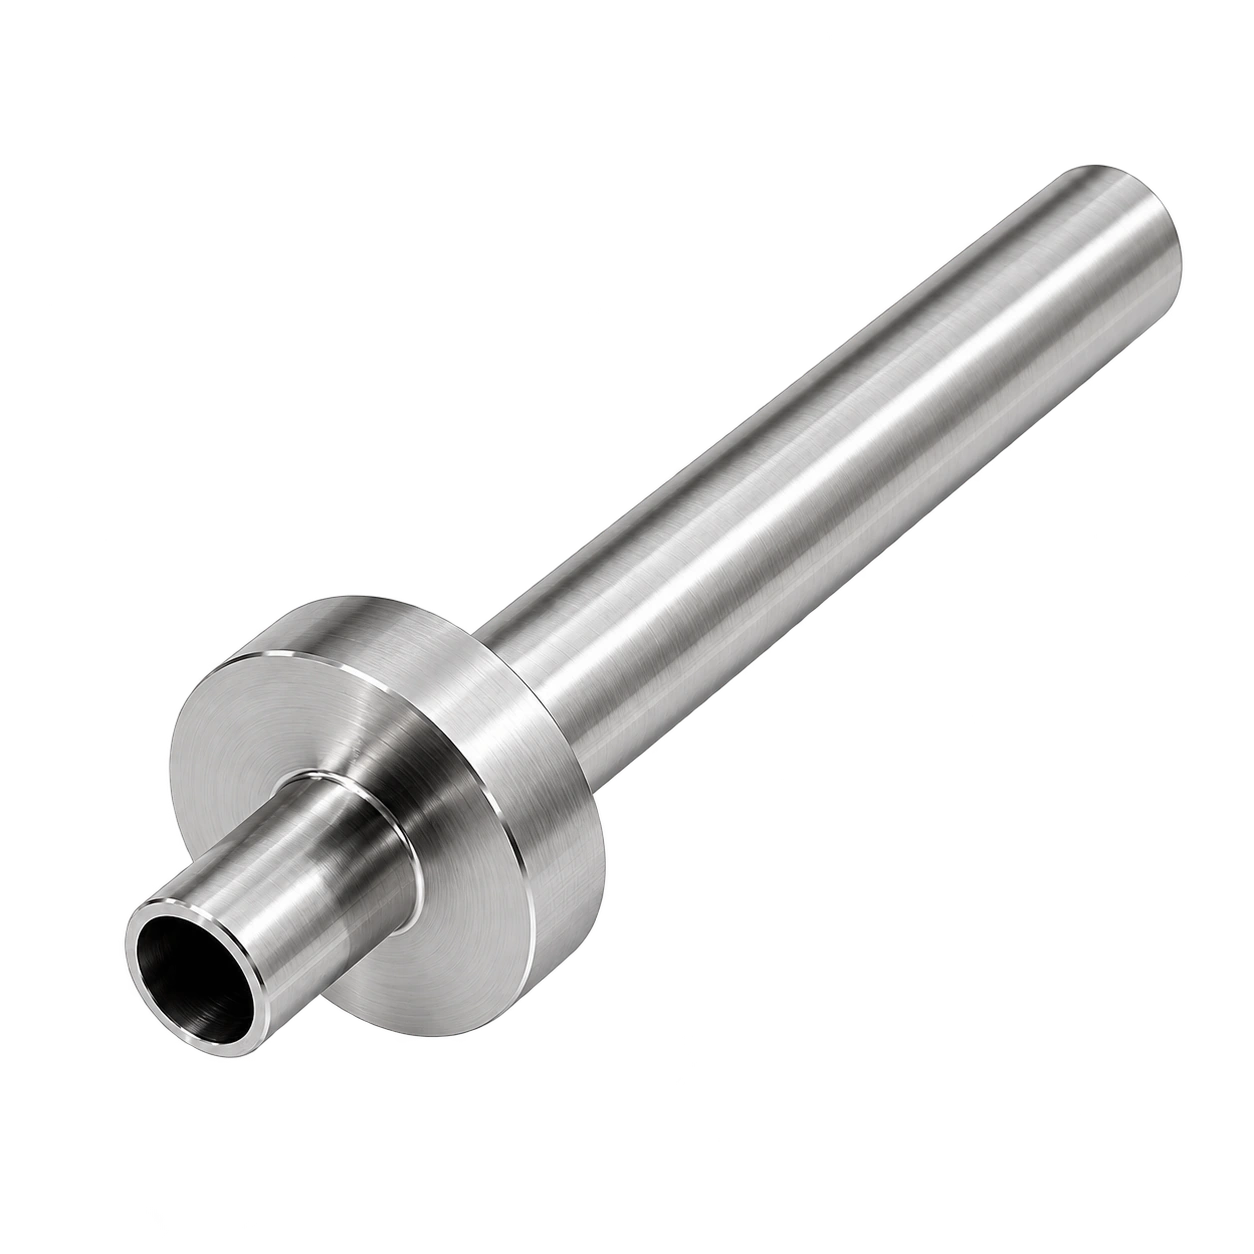
긴 중공 축에 원형 플랜지가 더해진 부품입니다. 축 끝의 개방된 홀과 플랜지를 기준으로 달라지는 외경 단차를 보여줍니다. 칼라 위치와 긴 중공 축의 정렬를 중심으로 도면과 조립 조건을 검토합니다.
Long hollow shafts combine open ends, circular flanges and changes in outside diameter. Drawing review focuses on collar location and long hollow-shank alignment.
길게 이어지는 축부
Extended cylindrical shank
원형 칼라
Circular collar
끝단 개구와 내부 형상
End opening and internal geometry
제품 형상과 기능 구간
Geometry & functional features
원통 축과 칼라 지지면을 기준으로 칼라 위치와 긴 중공 축의 정렬를 나눠 살펴봅니다.
Review collar location and long hollow-shank alignment from the cylindrical axis and collar seating face.
외형과 기능 구간
External geometry
긴 중공 축에 원형 플랜지가 더해진 부품입니다. 축 끝의 개방된 홀과 플랜지를 기준으로 달라지는 외경 단차를 보여줍니다. 칼라 위치와 긴 중공 축의 정렬를 중심으로 도면과 조립 조건을 검토합니다.
Long hollow shafts combine open ends, circular flanges and changes in outside diameter. Drawing review focuses on collar location and long hollow-shank alignment.
VISIBLE GEOMETRY
개방 홀 · 긴 축 · 원형 플랜지
01
길게 이어지는 축부
Extended cylindrical shank
긴 원통 구간과 짧은 끝단이 칼라 양쪽에 놓입니다. 지지 또는 삽입되는 구간의 길이를 따로 정하고, 긴 외경을 한 단면의 측정만으로 판단하지 않도록 측정 위치를 계획합니다.
A long shank and shorter end lie on opposite sides of the collar. Identify their supported or inserted lengths and plan measurement locations along the extended cylinder.
02
원형 칼라
Circular collar
축보다 넓은 얇은 칼라는 축 방향 위치를 구분하는 형상입니다. 칼라의 바깥지름과 두께, 실제 닿는 면을 분리하고 그 면에서 양 끝단까지의 거리를 확인합니다.
The thin, enlarged collar distinguishes an axial location. Separate its diameter, thickness and seating face, then reference both end positions from that face.
03
끝단 개구와 내부 형상
End opening and internal geometry
원통 끝에서 개구가 보이며 외부 축과 구분되는 내공 조건이 필요합니다. 보이는 입구 크기만으로 내부가 같은 지름으로 관통한다고 가정하지 않고 깊이와 단차를 단면도로 확인합니다.
An opening is visible at the cylinder end and requires a separate internal specification. Entrance size alone does not establish a uniform through-bore; confirm depth and steps in section.
04
칼라 양쪽의 길이
Lengths on either side of the collar
긴 축과 짧은 끝단의 길이는 서로 다른 조립 구간을 형성합니다. 전체 길이와 칼라 위치를 독립적으로 검토해 끝단 깊이와 멈춤 위치가 동시에 맞는지 확인합니다.
Long and short projections form different assembly regions. Review overall length and collar location separately so insertion depth and stop position can both be satisfied.
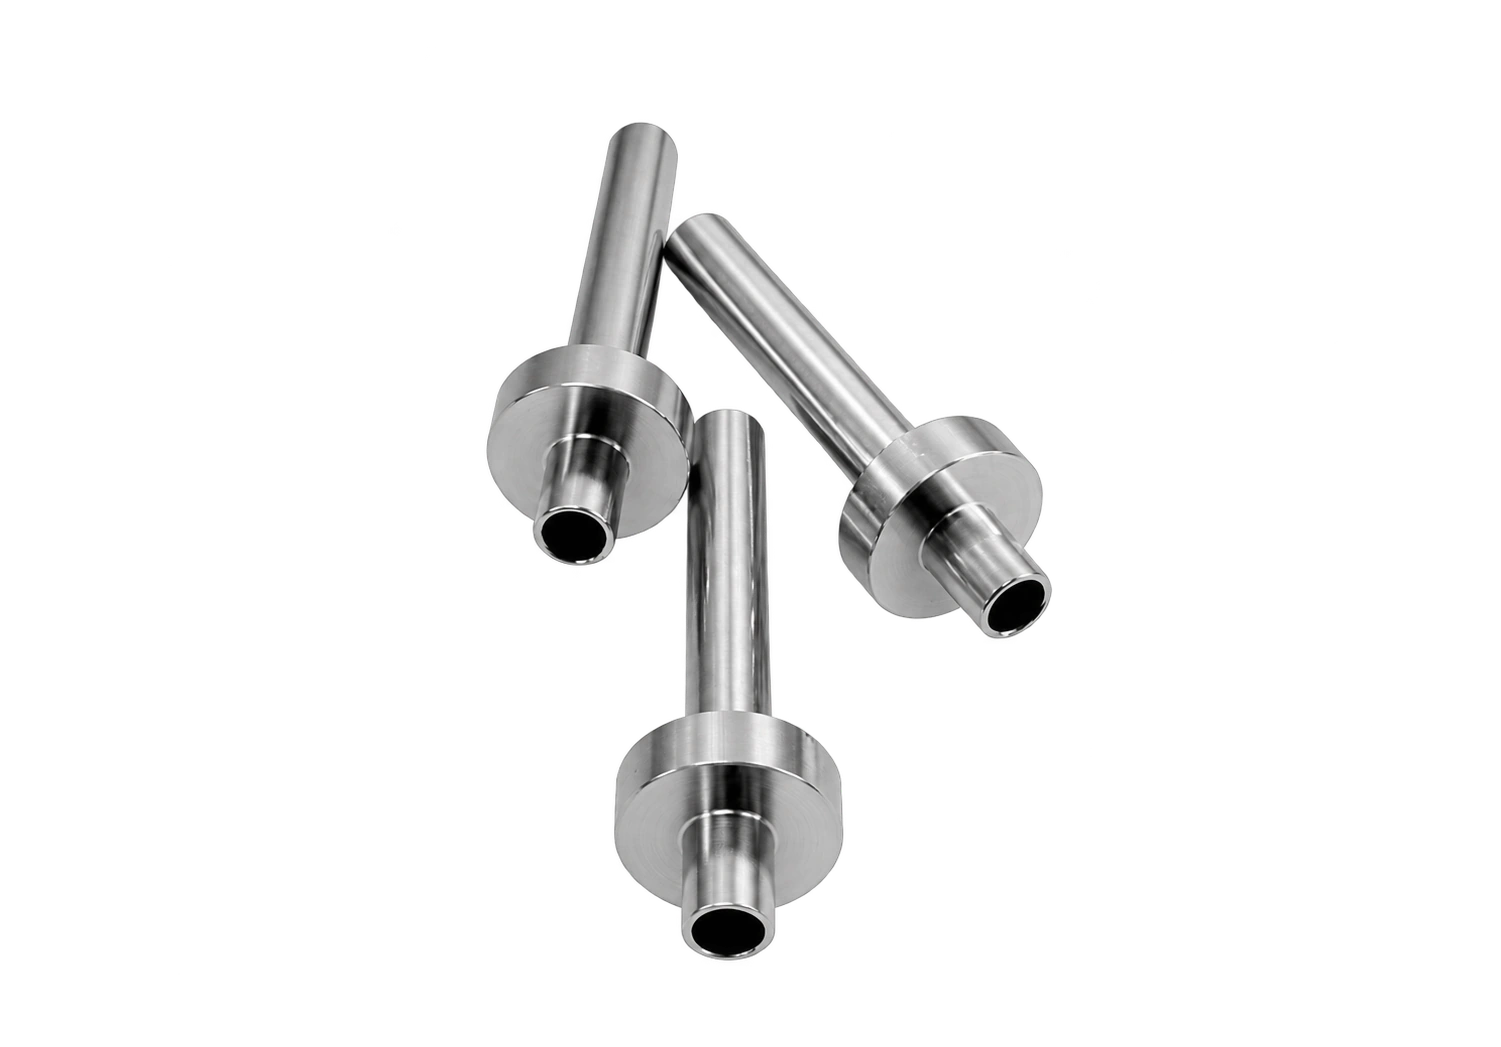
원본에서 확인되는 형상
Source geometry
원본 외관을 바탕으로 한 비례 모델입니다. 실제 치수·공차·소재와 가려진 내부 형상은 승인도면을 따릅니다.
A proportional study of the reference appearance. Production dimensions, tolerances, material and hidden geometry follow the approved drawing.
입체 형상과 설계 항목
3D geometry & design terms
원통 축과 칼라 지지면에서 주요 형상의 위치와 방향을 확인합니다. 기호는 검토 항목을 구분하며 생산 치수를 나타내지 않습니다.
Locate features from the cylindrical axis and collar seating face. Symbols identify review dimensions, not production values.
전체 길이 / Overall length
긴 축 외경 / Long-shank diameter
끝단 개구 지름 / End opening diameter
칼라 외경 / Collar diameter
칼라 두께 / Collar thickness
긴 축 길이 / Long-shank length
짧은 끝단 길이 / Short-end length
끝단 모따기 / End chamfer
원본 외관을 바탕으로 한 비례 모델입니다. 실제 치수·공차·소재와 가려진 내부 형상은 승인도면을 따릅니다.
A proportional study of the reference appearance. Production dimensions, tolerances, material and hidden geometry follow the approved drawing.
도면과 제작 사양
Drawing & manufacturing inputs
제품 구분
중공 플랜지 샤프트 / Hollow flanged shafts
확인 형상
개방 홀 · 긴 축 · 원형 플랜지
전체 길이
L · 승인도면 기준
L · Defined by the approved drawing
긴 축 외경
D · 승인도면 기준
D · Defined by the approved drawing
끝단 개구 지름
d · 승인도면 기준
d · Defined by the approved drawing
칼라 외경
Dc · 승인도면 기준
Dc · Defined by the approved drawing
칼라 두께
T · 승인도면 기준
T · Defined by the approved drawing
긴 축 길이
La · 승인도면 기준
La · Defined by the approved drawing
짧은 끝단 길이
Lb · 승인도면 기준
Lb · Defined by the approved drawing
끝단 모따기
C · 승인도면 기준
C · Defined by the approved drawing
가공 검토와 제조 흐름
Machining route & process planning
형상과 기능면을 기준으로 구성한 가공 검토 흐름입니다. 세부 순서와 공구·고정 방식은 소재, 수량과 도면 조건에 따라 정합니다.
A geometry-led machining review. Sequencing, tooling and workholding depend on material, quantity and drawing requirements.
도면과 기준 확인
Drawing and datum review
원통 축과 칼라 지지면을 기준으로 형상과 조립 조건을 정리합니다. 칼라 위치와 긴 중공 축의 정렬에 해당하는 치수를 도면에서 구분합니다.
Establish the cylindrical axis and collar seating face and identify drawing requirements for collar location and long hollow-shank alignment.
소재와 공급 상태 검토
Material and stock review
소재 등급과 공급 형상, 후처리 요구를 확인합니다. 절삭 조건은 확정된 소재 자료와 가공 구간에 연결합니다.
Confirm material grade, stock form and finishing requirements; connect machining conditions to approved material data.
물림과 가공 기준 설정
Workholding and setup
원통 축과 칼라 지지면이 공정 중 이어지도록 물림 위치와 공구 접근을 검토합니다. 가공면과 지지면이 겹치는 구간은 재물림 순서에 반영합니다.
Plan workholding and access while maintaining the cylindrical axis and collar seating face; account for surfaces unavailable in the initial setup.
긴 축 기준 가공
Machine the long-shank reference
초기 형상에서 가공 기준을 확보하고 필요한 면과 단차를 구분합니다. 소재를 잡는 위치와 가공 후 남는 형상을 함께 검토합니다.
Establish the machining reference and identify required faces and shoulders, considering workholding and the remaining geometry.
칼라·끝단 단차 가공
Machine collar and end steps
도면의 위치 기준에 맞춰 가공 범위를 정하고 공구가 접근하는 방향을 확인합니다. 연결부의 간섭과 남는 단면을 함께 살펴봅니다.
Define the machining extent from drawing datums and review tool direction, transition access and remaining sections.
내공 조건에 따른 홀 가공
Machine the specified internal opening
주요 기능 형상의 크기와 위치, 유효 길이를 정리합니다. 상대 부품과 연결되는 구간은 도면의 조립 요구에 맞춰 검토합니다.
Define the size, position and usable extent of functional geometry and relate the interface to assembly requirements.
단면·입구 마무리
Finish faces and entrances
마지막 가공으로 형성되는 면과 입구·끝단의 버를 확인합니다. 모서리 마무리 범위와 최종 치수 판정 상태를 연결합니다.
Check final faces and residual burrs at entrances or ends and connect edge-finishing requirements with the final inspection condition.
치수 확인과 식별
Verification and identification
칼라 위치와 긴 중공 축의 정렬를 승인도면의 검사 항목과 연결해 확인합니다. 측정 위치와 기준, 적용된 도면 개정 정보를 함께 기록합니다.
Verify collar location and long hollow-shank alignment against the inspection plan and record measurement references and drawing revision.
형상을 구현하는 가공 기술
Machining & verification methods
칼라 위치와 긴 중공 축의 정렬를 만드는 공정과 형상을 확인하는 검사를 연결합니다.
Connect the operations and inspections used to establish collar location and long hollow-shank alignment.
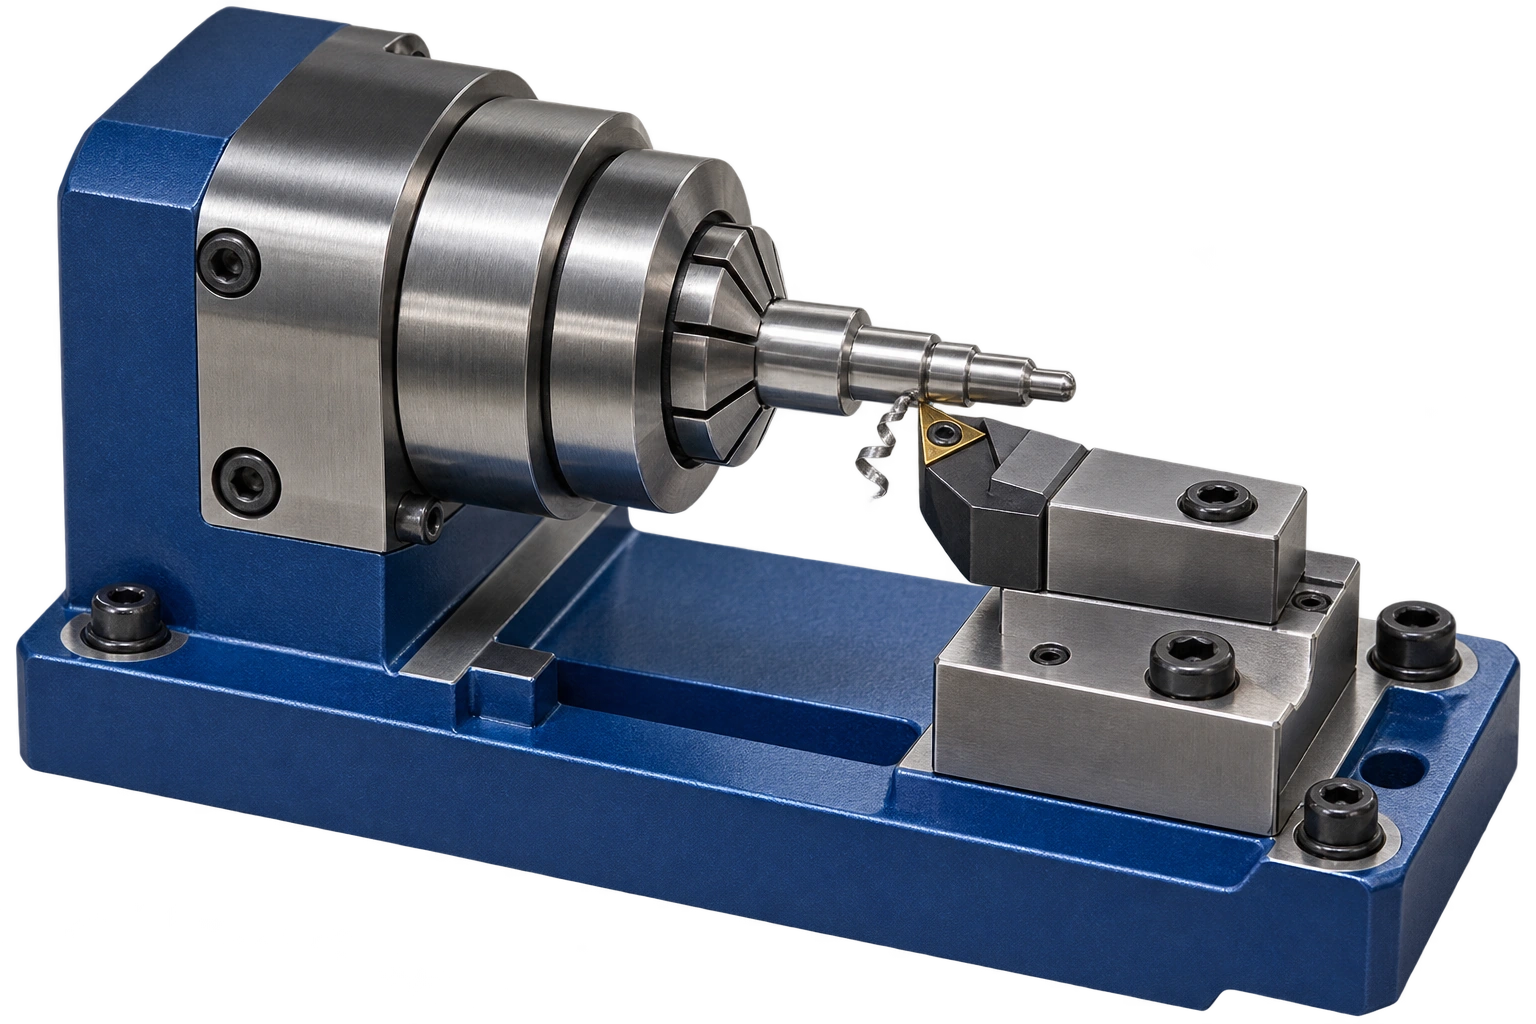
01
외경과 단차 가공
Profile turning
원통 축과 칼라 지지면을 유지하며 외경 구간과 숄더의 위치를 검토합니다. 돌출 길이와 지지 조건, 연결부의 공구 접근을 함께 확인합니다.
Maintain the cylindrical axis and collar seating face while reviewing diameter regions and shoulders, including overhang, support and access.
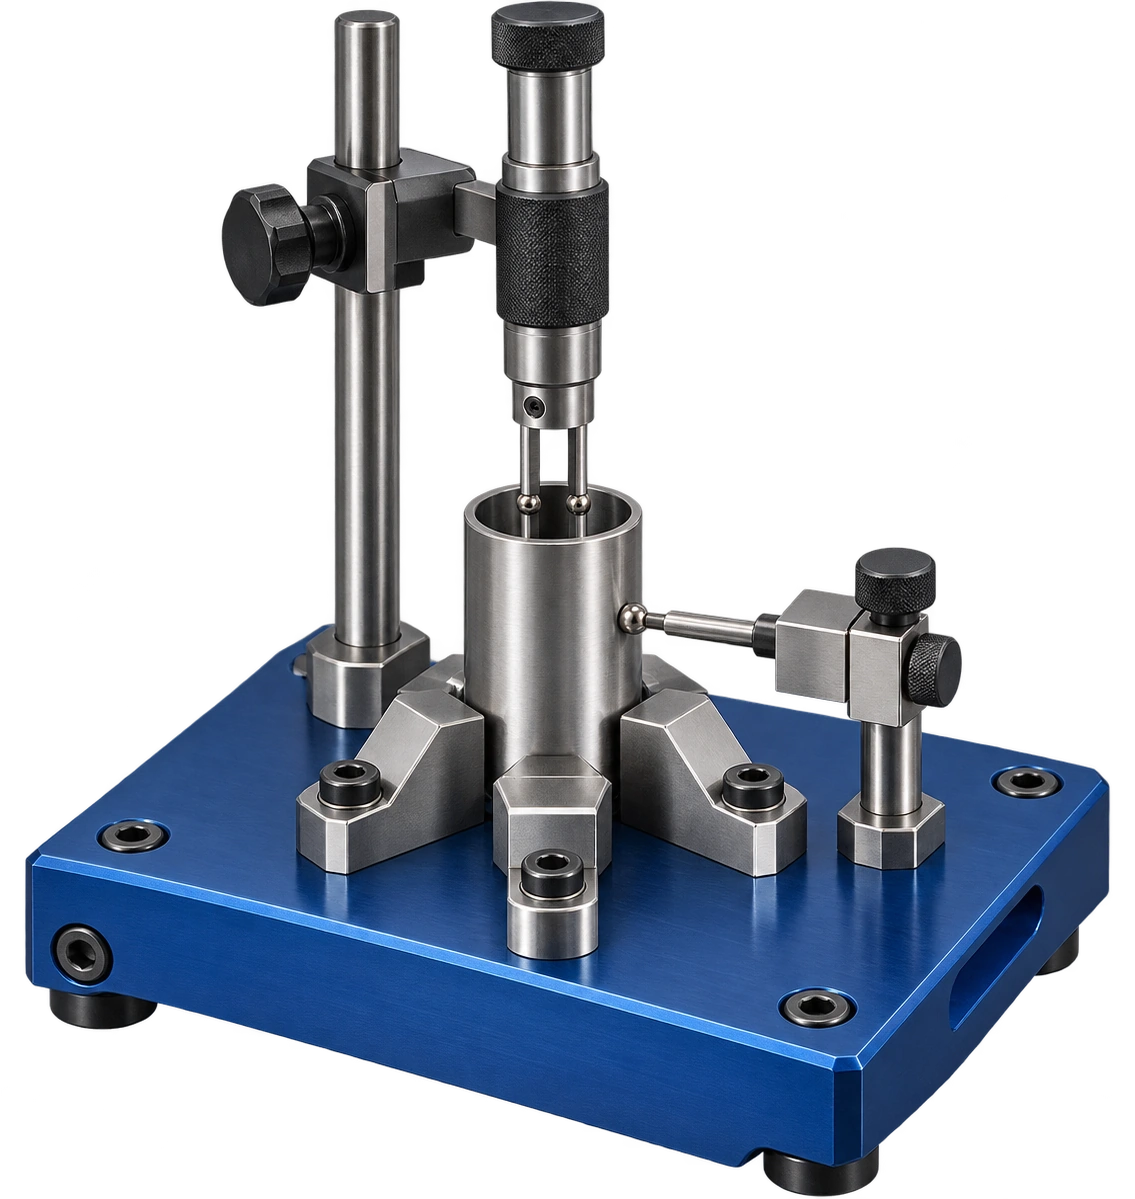
02
내경과 개구 확인
Bore measurement
내경과 개구는 외경과 별도의 측정 항목으로 정리합니다. 깊이와 방향별 측정 위치를 지정하고 접근 가능한 게이지와 측정 방식을 검토합니다.
Treat bores and openings separately from outside diameters. Specify measurement depths and directions and select accessible methods.
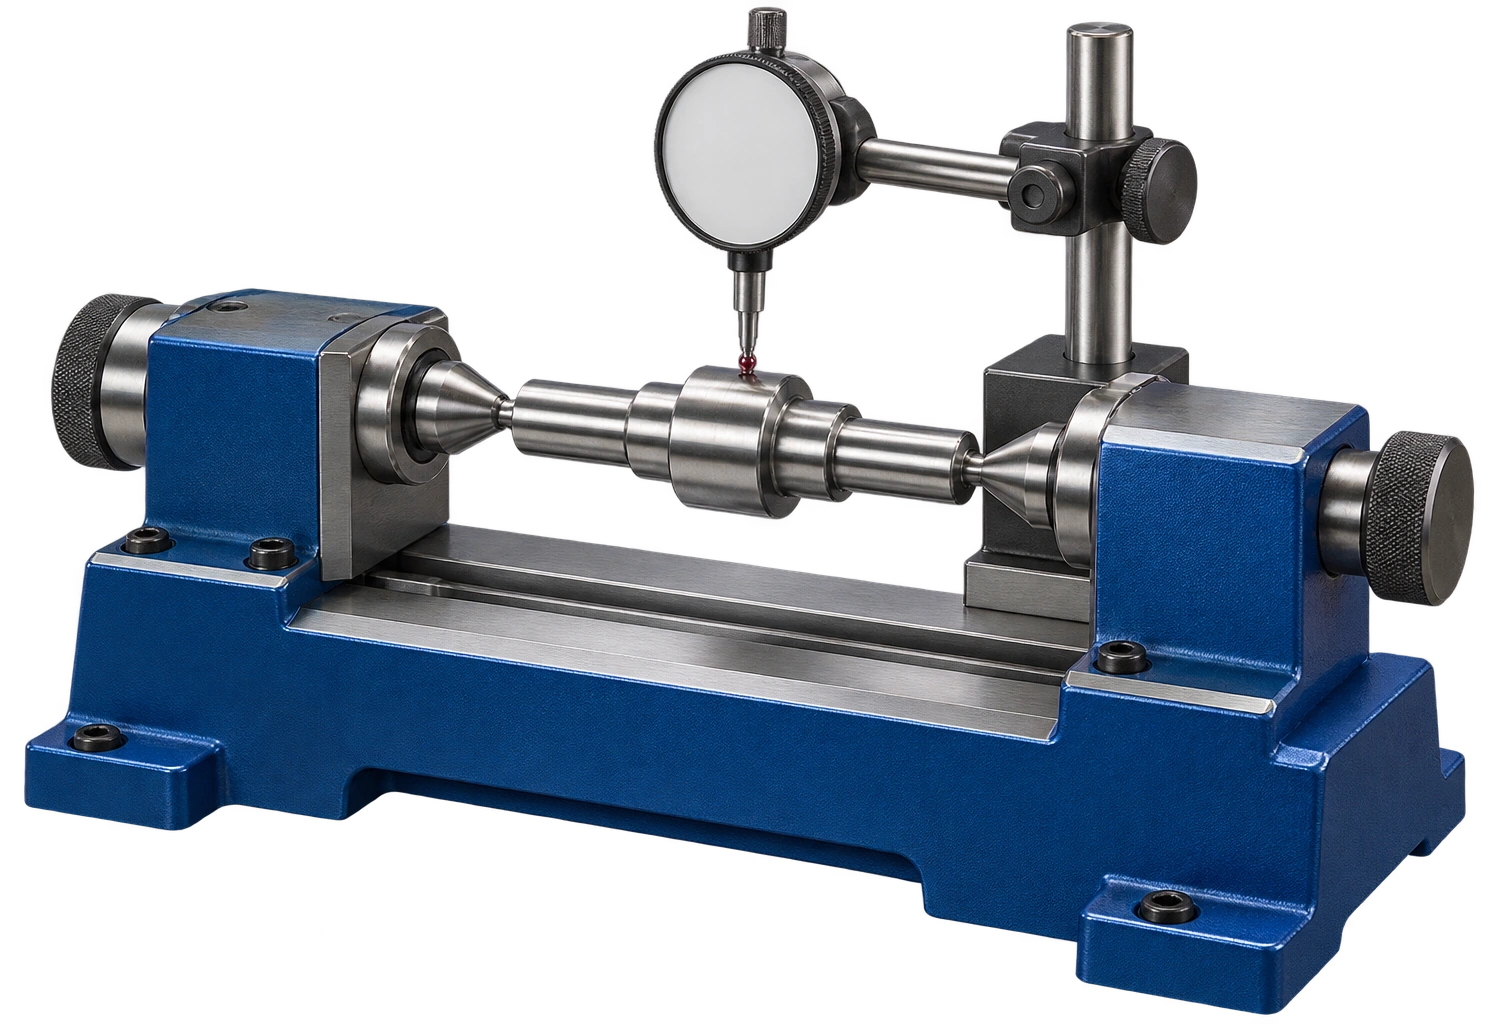
03
회전 기준 확인
Rotational reference inspection
원통 축과 칼라 지지면에 맞춘 지지 조건에서 기능면의 흔들림을 확인하는 경로입니다. 측정 위치와 지지 기준을 정하고 개별 단면 형상과 구분해 기록합니다.
Review functional-surface variation with support aligned to the cylindrical axis and collar seating face. Define measurement locations and distinguish local section form.
공정 이미지는 제작·측정 원리를 설명하는 개념 시각화입니다. 적용 공정과 장비 구성은 승인도면과 제작 조건에 따라 검토합니다.
Process illustrations describe manufacturing and measurement principles. The production route is reviewed against the approved drawing and manufacturing conditions.
상대 부품과 조립 조건
Mating parts & assembly conditions
긴 축이 들어가는 구간과 칼라가 멈추는 면를 바탕으로 방향, 지지와 조립 여유를 정리합니다.
Review orientation, support and clearance around the inserted shank region and collar stop face.
ENGINEERING RELATION
지름 여유와 반경 여유
Cᴅ = Dₕ − Dₛ ; Cᵣ = Cᴅ / 2
Dₕ는 상대 홀 지름, Dₛ는 삽입 축 지름입니다. Cᴅ는 지름 방향 여유이고 Cᵣ는 축이 동심일 때 한쪽 반경 방향 여유입니다.
Dₕ is the mating-hole diameter and Dₛ the inserted-shaft diameter. Cᴅ is diametral clearance; Cᵣ is the one-sided radial clearance when concentric.
실제 최소·최대 여유는 양쪽 부품의 허용 치수로 계산합니다. 음수 값은 지름 간섭을 뜻하며 탄성 변형이나 조립력을 계산하지 않습니다.
Calculate minimum and maximum clearance from both parts’ limits. A negative value indicates diametral interference; the relation does not calculate deformation or assembly force.
조립 방향
Assembly orientation
긴 축이 들어가는 구간과 칼라가 멈추는 면를 먼저 정리하고 상대 부품의 기준과 연결합니다. 외관이 비슷해도 실제 맞물리는 구간은 도면으로 구분합니다.
Establish the inserted shank region and collar stop face and relate it to mating-part datums.
닿는 면과 여유
Seating and clearance
원통 축과 칼라 지지면 주위에서 닿는 면과 비접촉 구간을 나눕니다. 조립 간격과 삽입 깊이는 상대 부품 치수와 함께 검토합니다.
Separate seating and clearance regions around the cylindrical axis and collar seating face and review insertion depth with mating dimensions.
조립 후 확인
Post-assembly check
단품 형상과 조립 후 위치 확인을 구분합니다. 필요한 고정 상태와 움직임, 간섭 여부는 실제 조립 조건에서 확인합니다.
Separate part verification from assembly checks and evaluate retention, movement and interference in the intended configuration.
형상과 기능의 관계
Geometry & functional relationships
칼라 연결부와 중공 축의 벽에 연결되는 힘의 경로와 접촉 조건을 검토합니다.
Review load paths and contact conditions around the collar transition and hollow-shaft wall.
단면의 변화
Section transitions
칼라 연결부와 중공 축의 벽을 중심으로 단면이 달라지는 위치를 확인합니다. 연결부 형상과 남는 단면은 하중 경로에 맞춰 검토합니다.
Review section changes around the collar transition and hollow-shaft wall and assess remaining geometry against the load path.
접촉과 지지
Contact and support
긴 축이 들어가는 구간과 칼라가 멈추는 면에서 실제 닿는 면과 지지 범위를 구분합니다. 지름이나 길이 한 항목만으로 조립 상태를 판단하지 않습니다.
Distinguish contact and support regions for the inserted shank region and collar stop face rather than assessing assembly from one dimension alone.
기능 검증 조건
Functional verification
실제 하중 방향과 반복 동작, 사용 환경을 검토 항목에 연결합니다. 필요한 성능값은 소재와 상대 부품, 시험 조건을 정한 뒤 확인합니다.
Define load direction, repeated operation and environment; establish performance using the specified material, mating parts and test conditions.
ENGINEERING RELATION
중공 원형 단면의 면적
Aₙ = π(Dₒ² − Dᵢ²) / 4
Dₒ는 해당 단면의 바깥지름, Dᵢ는 안지름이며 Aₙ은 동심 원형 중공 단면의 기하학적 면적입니다. 두 지름은 같은 단위로 사용합니다.
Dₒ is the outside diameter and Dᵢ the inside diameter of the same section. Aₙ is the geometric area of a concentric annular section, using consistent units.
모따기·홈·나사·편심·단차가 없는 단면에 적용합니다. 이 값만으로 강도나 실제 접촉 면적을 정하지 않습니다.
Applies to a section without chamfers, slots, threads, eccentricity or steps. Area alone does not determine strength or actual contact area.
소재와 표면 관리
Material & surface requirements
기능면의 요구와 외관 표현을 구분하고 최종 완성 상태를 기준으로 표면 조건을 정리합니다.
Separate functional-surface requirements from appearance and define the final finished condition.
소재와 외관
Material and appearance
색상과 광택은 원본 형상을 표현하는 외관 정보입니다. 제작 소재와 공급 상태는 도면, 소재 규격과 성적서로 구분합니다.
Colour and sheen describe the reference appearance. Define production material and condition through drawings, specifications and certificates.
기능면과 마무리
Functional finish
칼라 위치와 긴 중공 축의 정렬에 관련된 면의 표면 요구를 구분합니다. 모따기와 버 제거 범위는 형상 치수 및 조립 방향과 함께 지정합니다.
Specify surface requirements for collar location and long hollow-shank alignment and relate edge finishing to geometry and assembly direction.
후처리와 치수
Treatment and dimensions
표면처리나 열처리가 필요한 경우 적용 범위와 공정 순서를 정리합니다. 최종 검사 기준이 처리 전·후 중 어느 상태인지 구분합니다.
When treatment is specified, define coverage and sequence and identify whether inspection applies before or after treatment.
품질 검토와 원인 구분
Quality review & defect analysis
도면 기준을 측정 위치, 결과 기록과 제품 식별에 연결합니다.
Connect drawing requirements to measurement locations, records and product identification.
도면 개정 관리
Drawing revision
형상과 검사 항목, 소재 조건이 같은 도면 개정을 참조하도록 정리합니다. 변경된 기능면은 재검토 항목으로 구분합니다.
Align geometry, inspection and material requirements with one drawing revision and review changed functional features.
기준 위치 기록
Measurement references
원통 축과 칼라 지지면에서 측정 위치와 방향을 지정합니다. 반복 측정은 같은 지지 조건을 사용하도록 계획합니다.
Specify measurement positions and directions from the cylindrical axis and collar seating face and maintain consistent support.
형상과 외관 구분
Geometry and appearance
치수·형상 결과와 표면의 찍힘, 버, 오염을 서로 다른 항목으로 기록합니다. 외관 판정 기준은 사용 부위에 맞춰 정리합니다.
Record geometry separately from dents, burrs or contamination and define appearance criteria for the intended interface.
제품 식별과 보호
Identification and protection
중공 플랜지 샤프트의 형상이 취급과 포장 과정에서 손상되지 않도록 접촉 위치를 검토합니다. 로트와 검사 기록을 연결할 식별 조건을 정리합니다.
Review handling contact points to protect hollow flanged shafts geometry and connect lot identification with inspection records.
검사 항목과 기록 기준
Inspection characteristics & records
아래 표는 형상별 검사 계획 항목입니다. 측정 방식과 허용 기준은 승인도면에 맞춰 확정합니다.
These are geometry-specific inspection planning items. Final methods and acceptance criteria follow the approved drawing.
검사 특성 / CHARACTERISTIC
측정 접근 / METHOD
기록 기준 / RECORD
전체 길이
Overall length
마이크로미터·높이·영상 측정 검토
Review micrometer, height or optical measurement
승인도면의 전체 길이 및 연결된 형상·위치 요구
Approved overall length and associated form or location requirements
긴 축 외경
Long-shank diameter
치수·윤곽 측정 검토
Review dimensional and profile measurement
승인도면의 긴 축 외경 및 연결된 형상·위치 요구
Approved long-shank diameter and associated form or location requirements
끝단 개구 지름
End opening diameter
내경 게이지·핀 게이지·영상 측정 검토
Review bore gauge, pin gauge or optical measurement
승인도면의 끝단 개구 지름 및 연결된 형상·위치 요구
Approved end opening diameter and associated form or location requirements
칼라 외경
Collar diameter
치수·윤곽 측정 검토
Review dimensional and profile measurement
승인도면의 칼라 외경 및 연결된 형상·위치 요구
Approved collar diameter and associated form or location requirements
칼라 두께
Collar thickness
마이크로미터·높이·영상 측정 검토
Review micrometer, height or optical measurement
승인도면의 칼라 두께 및 연결된 형상·위치 요구
Approved collar thickness and associated form or location requirements
긴 축 길이
Long-shank length
마이크로미터·높이·영상 측정 검토
Review micrometer, height or optical measurement
승인도면의 긴 축 길이 및 연결된 형상·위치 요구
Approved long-shank length and associated form or location requirements
짧은 끝단 길이
Short-end length
마이크로미터·높이·영상 측정 검토
Review micrometer, height or optical measurement
승인도면의 짧은 끝단 길이 및 연결된 형상·위치 요구
Approved short-end length and associated form or location requirements
끝단 모따기
End chamfer
치수·윤곽 측정 검토
Review dimensional and profile measurement
승인도면의 끝단 모따기 및 연결된 형상·위치 요구
Approved end chamfer and associated form or location requirements
적용 기능과 사용 조건
Functional applications & service conditions
형상에 따른 적용 검토 분야입니다. 실제 사용 적합성은 상대 부품과 요구 성능을 기준으로 확인합니다.
Geometry-based application review areas; confirm suitability against actual mating parts and performance requirements.
긴 원통부의 삽입과 안내
Long-shank insertion and guidance
긴 외경이 상대 구멍으로 들어가는 구조에서는 길이에 따른 조립 여유와 지지 위치를 함께 검토합니다. 칼라에 닿기 전 축 끝에서 간섭하는 조건을 구분합니다.
For a long shank entering a hole, review clearance along its length and support locations. Distinguish tip interference from proper collar seating.
칼라 기준의 축 방향 위치
Collar-referenced axial location
칼라 면을 멈춤 기준으로 사용하는 배치에서는 칼라 양쪽 길이가 각각 다른 부품과 연결됩니다. 긴 쪽과 짧은 쪽을 구분해 설치 방향과 삽입 깊이를 관리합니다.
When the collar sets the stop position, its two projections may interface with different parts. Distinguish long and short sides to control orientation and insertion depth.
내부 공간이 필요한 축 형상
Shafts requiring internal space
내공이 필요한 부품에서는 외부 축 강성 검토와 내부 통로 조건을 나누어 정리합니다. 개구가 관통하는지, 내부 단차가 있는지는 사진이 아닌 승인 단면도에서 확인합니다.
For an internally open shaft, separate outer structural requirements from the internal passage. Confirm through depth and internal steps from an approved section view.
도면에서 완성 형상까지
From drawing to finished geometry
중공 플랜지 샤프트의 칼라 위치와 긴 중공 축의 정렬를 기준으로 가공과 조립·검사를 연결합니다. 검토 도면과 수량, 소재 및 표면 조건을 함께 정리하여 필요한 기능면과 확인 범위를 명확히 합니다.
Connect machining, assembly and inspection through collar location and long hollow-shank alignment. Review drawing, quantity, material and surface requirements together.
사양 검토에 필요한 자료
Required information
01
최신 개정 2D 도면과 가능한 3D 데이터
02
소재 규격과 공급 상태
03
기준면·기준축과 주요 기능 치수
04
상대 부품의 결합 형상과 조립 방향
05
표면·후처리 및 모서리 마무리 조건
06
수량·검사 기록·포장 조건